 Small batches, high standards. Our rapid prototyping service makes validation faster and easier —
 EN

How Much Do Automotive Stampings Cost? Piece Price vs. Tooling
How Much Do Automotive Stampings Cost? Piece Price vs. Tooling
The cost of a custom automotive stamping has two parts: a one-time tooling investment and a recurring piece price. Based on our own quoting data, a die for a simple blanked or pierced part typically costs $1,000–5,000, a medium progressive die for brackets, retainers and mounting plates $10,000–30,000, and a complex progressive die for chassis and suspension parts $20,000–50,000 or more. The piece price is then driven mainly by material, press time and scrap.
Put simply: Total cost = Tooling + (Piece price × Volume). The rest of this article explains how each half is built up, which die suits which volume, and why two suppliers can quote the same part very differently.
Typical Tooling Investment by Part Type
These are reference ranges from our tool room for common automotive stamping dies. Your part will be quoted on its own drawing, but this is where most projects land.
|
Die type |
Typical parts |
Reference price (USD) |
Typical annual volume |
|
Simple blanking or piercing die |
Washers, flat plates, simple brackets |
$1,000–5,000 |
Up to ~100,000 |
|
Single-operation forming die |
Bent, flanged and simple formed parts |
$2,000–8,000 |
10,000–100,000 |
|
Compound die |
Precision blanks, washers, flanges |
$4,000–12,000 |
50,000–300,000 |
|
Small progressive die |
Small precision automotive stampings |
$5,000–15,000 |
100,000–1,000,000 |
|
Medium progressive die |
Retainers, brackets, mounting plates |
$10,000–30,000 |
100,000–1,000,000+ |
|
Complex progressive die |
Chassis brackets, suspension parts |
$20,000–50,000+ |
300,000–2,000,000 |
|
Transfer die |
Large chassis and structural parts |
$30,000–100,000+ |
100,000–1,000,000+ |
For deep-drawing dies, high-complexity progressive dies and large transfer dies, see our full breakdown of stamping die cost.
Tooling vs. Piece Price: Why Stamping Gets Cheaper With Volume
Stamping behaves differently from laser cutting or CNC machining. With those processes, the cost per part stays fairly flat whether you order 100 pieces or 10,000. With stamping, most of the money goes into the die up front, and after that each part costs very little to produce. The more parts the die makes, the smaller the tooling share in each one.
Tooling covers die design, die steel and machining, assembly, and the tryout phase where the die is adjusted until it produces parts to drawing. It is paid once.
Piece price covers material, press time, labour, secondary operations such as tapping, welding or coating, packaging and overhead. It is paid on every part.
How to Estimate the Piece Price
A manual estimate follows four steps. Simulation software can refine the numbers for complex geometry, but the logic is the same.
1. Net material cost
Start with the blank or strip area per part, multiplied by thickness and density, to get the gross weight. The skeleton left after stamping is scrap, and it has resale value.
Material cost = (Gross weight × Material price/kg) − (Scrap weight × Scrap value/kg)
For most steel stampings, material is the largest single share of the piece price, which is why strip layout and nesting matter so much. A better strip layout can lift material utilisation by several percentage points, and at high volume that is real money.
2. Press time
Each press has an hourly rate that rises with tonnage and bed size. Divide it by the number of parts produced per hour, and allow for coil changes, maintenance and downtime.
Press cost per part = Hourly rate ÷ (Strokes per hour × Parts per stroke × Efficiency)
3. Secondary operations
Tapping, welding, CNC machining of critical features, e-coating or plating, and packaging are added per part. When these are done in the same plant, handling and freight between suppliers disappear from the cost.
4. Tooling amortisation
Spread the die cost over the parts it will make across the programme.
Tooling cost per part = Die investment ÷ Lifetime volume
Take a medium progressive die at $20,000. Over 500,000 parts, it adds $0.04 to each part. Over 5,000 parts, the same die adds $4.00 — which is why low-volume projects usually need a different tooling strategy, not just a lower price.
Which Die Fits Your Volume
The most important cost decision is made before the die is designed: which type of tooling the volume justifies.
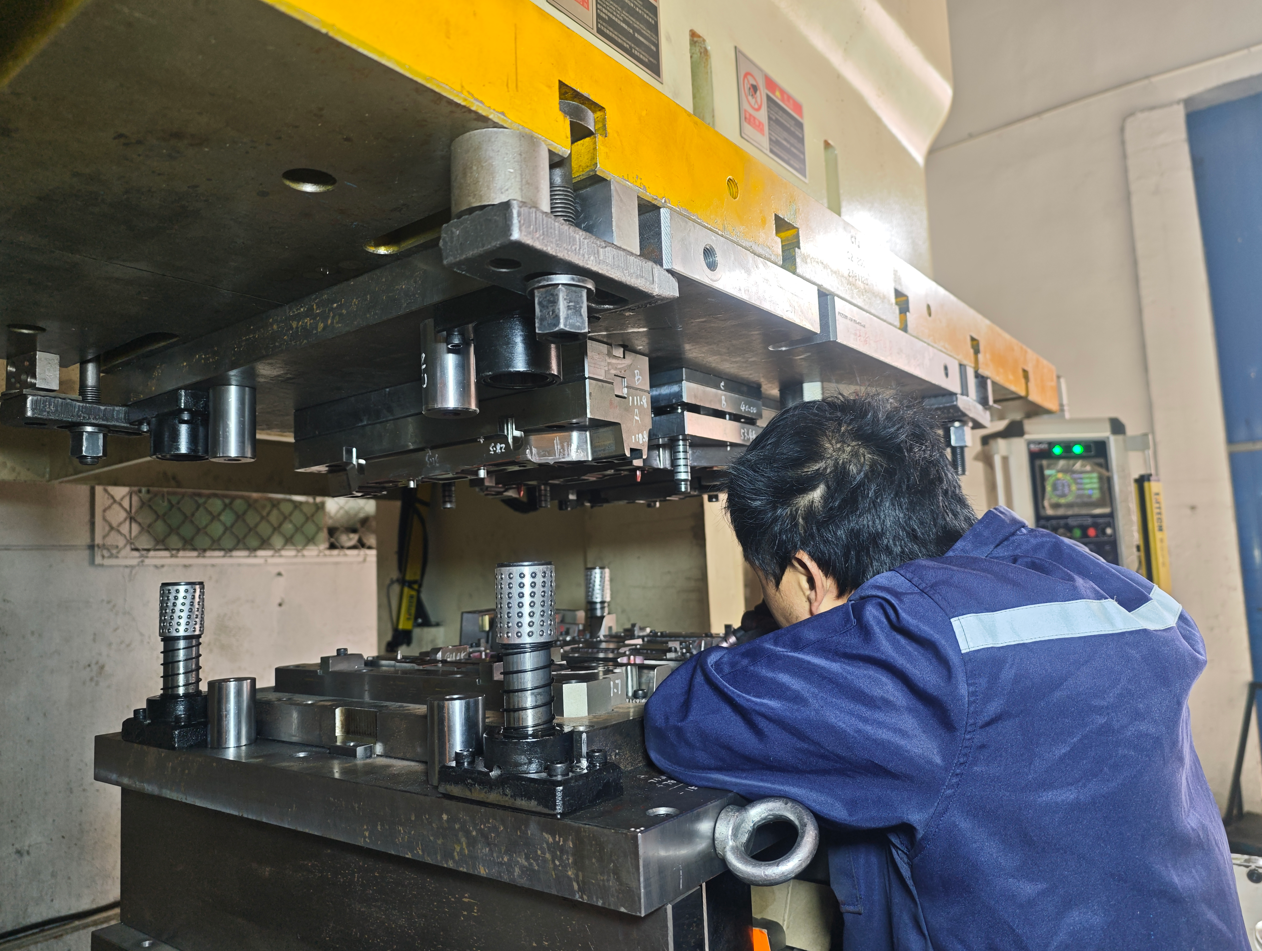
Simple blanking, piercing and single-operation dies suit volumes up to roughly 100,000 parts a year. Tooling is inexpensive, but each operation needs its own press stroke and handling, so the piece price is higher.
Progressive dies take over from around 100,000 parts a year. Several operations happen in one strip, one part drops with every stroke, and the piece price falls sharply. Complex chassis and suspension parts typically run on progressive dies at 300,000 to 2,000,000 parts a year.
Transfer dies suit parts that are too large or too deep for a progressive strip, typically at 100,000 parts a year and above.
For prototypes and validation batches, we use soft tooling or single-operation dies, so a programme can complete design and process validation before committing to hard tooling.
Why the Same Part Gets Very Different Quotes
Buyers are often surprised when two quotes for the same drawing differ by a factor of two or more. Usually neither supplier is wrong; they have assumed different things. These are the factors our engineers weigh most heavily:
|
Cost factor |
Impact |
Why it matters |
|
Part geometry |
Very high |
Complex forming needs more operations and mechanisms |
|
Number of stations |
Very high |
More stations mean more die components, machining and assembly |
|
Required tool life |
Very high |
Long-life dies need better steel, heat treatment and key inserts |
|
Cam mechanisms |
Very high |
Side-acting cams add mechanisms and machining cost |
|
Part size |
High |
Larger dies need more steel, bigger machines and more assembly space |
|
Material strength |
High |
High-strength steel needs stronger, more wear-resistant die design |
|
Tolerance |
High |
Tighter tolerances mean more precise machining and inspection |
|
Automation |
High |
Automatic feeding, transfer and in-die inspection add system complexity |
|
Customer standard |
High |
OEM and Tier-1 die standards, such as VW or Mercedes, add design and validation work |
|
Material thickness |
Medium |
Affects press force, die clearance and die structure |
|
Tryout and validation |
Medium |
Large or complex dies need more tryout and correction |
The practical lesson: compare quotes on the same assumptions. Ask each supplier to state the die type, number of stations, guaranteed tool life, die steel and the customer standard they quoted to. A cheaper die built for a shorter life is not a cheaper die.
How Material Changes the Cost
Low-carbon steels such as DC01 and DC04 are the baseline. HSLA grades such as S355MC and S420MC raise press force and need springback control. High-strength grades such as S460MC and S500MC, and advanced high-strength steels such as DP600, need stronger dies with better wear resistance and are more sensitive to cracking and springback. Stainless steel adds friction, galling and wear. Aluminium needs springback control and surface protection.
All of these push the die price up compared with low-carbon steel, and most of them also affect piece price through slower press speeds or more frequent die maintenance.
Design Choices That Lower Cost
Most of a part's cost is decided on the drawing. A few rules of thumb keep it down, though the right values always depend on the material:
Bend radius. Keep inside bend radii at or above the material thickness where the design allows, to avoid cracking without extra operations.
Hole-to-edge distance. Keep holes at least twice the material thickness from edges and bends, so they do not distort during forming.
Tolerances. Apply tight tolerances only to functional features. Standard stamping tolerances are far cheaper to hold than machining-grade tolerances, and a critical feature can be machined after stamping if it really needs it.
Nesting. Shapes that nest well on the strip waste less material. Small changes to an outline can lift material utilisation noticeably.
Costs That Don't Appear in the First Quote
Validation. Automotive parts need PPAP documentation, checking fixtures and CMM time. These are real costs, and they should be quoted, not discovered.
Die maintenance. Punches need sharpening and worn inserts need replacing. We typically budget 10% of the die value per year, depending on material and volume.
Engineering changes. A design change after the die is built means die modification. When the tool room and the press shop are in the same building, that change is faster and cheaper to make.
Logistics. When one supplier builds the die and also runs production, the die normally stays in that supplier's plant. That is how we work: our stamping dies are designed and built in-house in Ninghai and run on our own presses, so there is no heavy tooling to ship and no second supplier to coordinate when an adjustment is needed. The customer still owns the tooling they pay for; we store and maintain it for production.
How to Get an Accurate Quote
The more complete the RFQ, the closer the first quote will be to the final price. Include the 2D drawing and 3D model with revision level, material grade and thickness, annual and lifetime volume, the tool life you expect, coating requirements, critical-to-quality features, the PPAP level and any customer die standard.
If you are sourcing custom automotive stamping parts, send us your drawing. Our engineers return a technical analysis within 12 hours and a formal quotation within 24 hours, and we sign an NDA before any file is shared.
FAQ
How much do custom automotive stampings cost?
Cost is tooling plus piece price. Tooling typically ranges from $1,000–5,000 for a simple blanking die to $20,000–50,000 or more for a complex progressive die for chassis or suspension parts. The piece price depends mainly on material, press time, secondary operations and volume.
Is stamping cheaper than CNC machining?
At low volumes, usually not, because the die has to be paid for first. As volume grows, stamping becomes much cheaper per part, because a press produces a part in seconds while machining takes minutes. For prototypes and small batches, machining or soft tooling is often the better choice.
Does high-strength steel make stamping more expensive?
Yes. Grades such as S420MC, S500MC and DP600 need stronger, more wear-resistant dies and more careful springback control, which raises the die price and can raise the piece price through slower speeds and more maintenance.
Why do die quotes vary so much between suppliers?
Because suppliers assume different die types, station counts, tool life, die steel and customer standards. Compare quotes on the same assumptions before comparing prices.
Who owns the stamping die?
The customer owns the tooling they pay for. We store and maintain it for production runs.
Written by: Xungui Xu
Reviewed by: Nansen, International Business Manager
Last updated: 2026.8.23